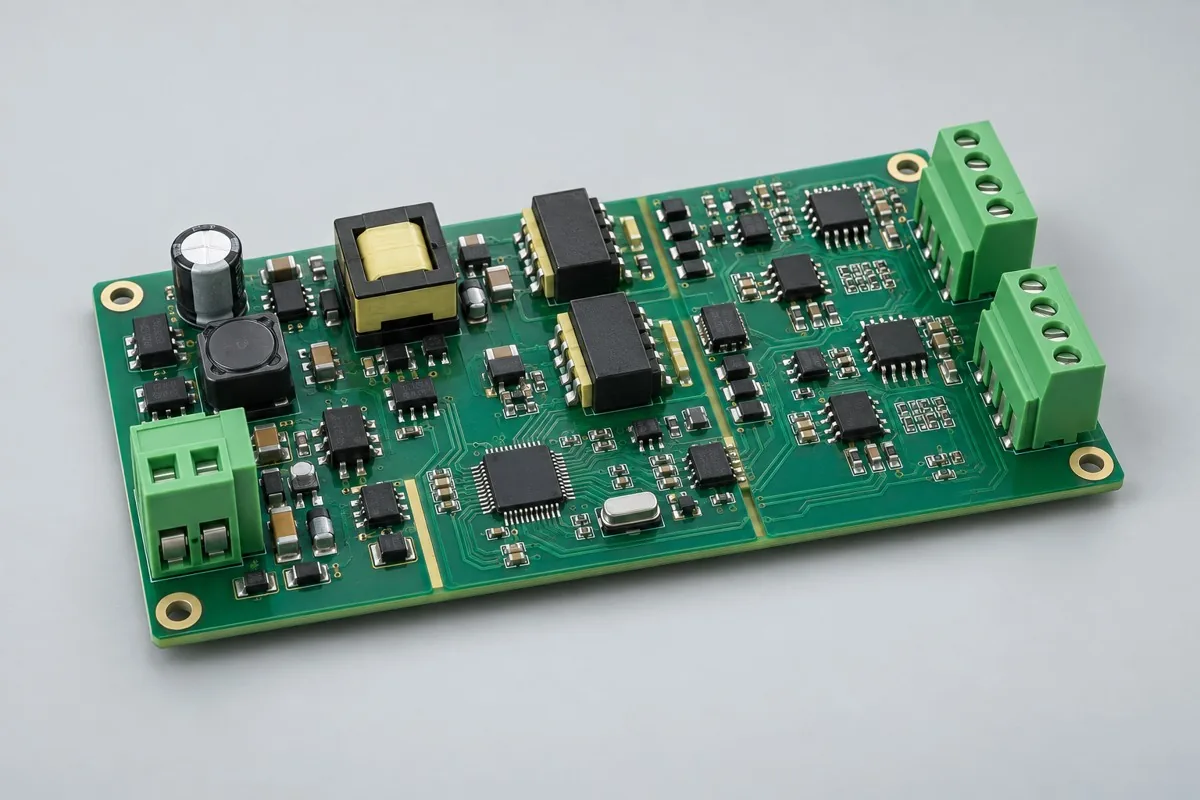
How much does industrial control PCB assembly cost? Why do acquisition and communication board quotes differ?
Quotes should separately itemize analog front ends and isolation components, subsequent terminal and interface installation, channel calibration or protocol fixtures, firmware identity, abnormal operating conditions, and functional testing. Separate initial order setup costs from recurring batch and per-board costs. For the same quantity, also align revisions, delivery configuration, and tax and shipping terms to determine whether price differences reflect configuration or excluded work.
Quotation terms depend on the approved files, quantity, material supply, tests and delivery requirements.
Prepare a structured RFQ or use the short inquiry form.
How do industrial A/D acquisition boards differ from communication interface boards?
A/D boards establish an input-output relationship for each channel, communication boards verify buses and isolation, and security boards verify events and alarms. Chip prices, calibration time, and test setups differ; board area alone cannot support a comparison.
Should I prioritize measurement range and accuracy or protocol and isolation for an industrial control board?
For acquisition, start with measurement range, accuracy, and sampling; for communication, protocols, interfaces, and isolation; for control, inputs/outputs and abnormal states. Selecting by field task is more effective than choosing by the industrial control board label.
Industrial control PCB assembly: order scope and acceptance
Define industrial control PCB assembly orders first by inputs/outputs and operating states. Analog I/O measurement, isolated communication, and alarm control require different materials, firmware, and fixtures. Implement high-current, isolation, or environmental targets through approved designs and test conditions.
A/D modules: measurement range/synchronization/data output; communication boards: bus/termination/isolation; monitoring boards: event rules/alarms/offline behavior.
Differences in assembly and test paths
Analog input calibration and reference sources, bus messages/addresses, and alarm state machines use different fixtures and records. Generic startup or single-port communication cannot replace them.
8 channel AD detection module
SMT → subsequent interface installation → programming → channel calibration. Locate reversed channels, reference source faults, and dropped output packets along separate path segments. Acceptance includes raw codes and converted data to prevent software compensation from hiding hardware faults. Recalibrate affected channels after analog front-end rework.
Isolated Industrial Communication Board
SMT → secondary terminal soldering → insulation area inspection → protocol testing. Reversed transceivers, incorrect termination, and duplicate addresses cause different communication failures. Acceptance requires boundary nodes and both ports operating together under a controlled bus load. One board's serial output does not establish field compatibility.
Smart security monitoring control board
SMT → secondary interface soldering → firmware/identity → states/network. Handle missed inputs, reversed alarms, lost logs, and duplicate identities separately. Acceptance covers normal and abnormal paths; an online network does not establish that all field inputs/local alarms work.
Convert field anomalies into test items
For acquisition boards, list measurement range/sampling; for communication boards, termination/bus; for security boards, alarm interlocks. Separately confirm disconnection, power loss, fault recovery, and field power for each type. An online device does not verify all functions. Signals and interfaces: define analog inputs, RS-485/CAN, or alarm I/O for each revision. Assembly inputs: approved BOM, pick-and-place files, terminal drawings, DNP positions and firmware. Define material-supply responsibilities and control changes through the agreed engineering-change process.
Component supply, quantity and delivery
Modules, boards, or assemblies with field harnesses can be quoted separately. For long-term supply, consider ADC/processor module/isolator lifecycles.
At ordering, align Gerber/BOM/pick-and-place files/DNP and assembly drawings, quantity, customer-supplied/procured material lists, and firmware verification. Delivery evidence includes calibration/address/event results and material lots. Do not transfer PCB factory capabilities into PCB assembly commitments. Confirm fees separately for stencil/carrier/fixture preparation, process operations, programming/calibration, and the supporting tests on this page. Agree on replenishment/attrition, excess materials, and change-related inventory first, then list delivery milestones after material readiness and scheduling are confirmed. Perform relevant regression testing for component/interface/mechanical/firmware changes, and record pilot issues separately from production release.
Material and Process Reference
Industrial control PCB assembly pricing and selection FAQ
How much does industrial control PCB assembly cost? Why do acquisition and communication board quotes differ?
For standard placement, first calculate board quantity × billable points per board × price per point + setup fee. A project-specific quotation requires review of the available files, quantity, materials, requested tests, delivery destination, taxes, shipping, and trade terms. This is a placement-only reference; bare PCBs, materials, and testing are charged separately. Any formula on this page organizes cost inputs; it is not a quoted rate.View cost items, calculation conditions, and sources.
How should I compare industrial control PCB assembly manufacturers' quotes?
Acquisition board quotes should list each channel's input points and calibration; communication boards should list bus, peer devices, and isolation conditions; security boards should list events and alarm states. Testing time and setups differ across these categories, so equal board area is not a sufficient comparison basis.
Is A/D acquisition calibration charged per channel or per board?
Align channel count, measurement range points, sources, and coefficient writing, then agree on the billing unit. Calibration setup differs from per-channel execution. Do not test one of eight channels and copy the result to the others.
Can an RS485 version become a CAN version by changing only the interface chip?
Check the transceiver, protection or isolation, terminals, and protocol. Approve the two BOMs and firmware revisions separately. Confirm bus peers and disconnection recovery for the new interface as well.
Why test communication loss if an industrial control board can connect to the network?
Normal communication does not define outputs, buffering, and recovery after network or power loss. Record faults against the state table, and identify peers and logs in the quote. A successful ping is not a complete release criterion.
How are materials made ready when we supply critical ADCs and isolators and authorize procurement of the rest?
Mark responsibilities, packaging, and replenishment contacts on the same BOM revision, and lock full models for precision and isolation parts. Check test impacts before authorized substitutions and lot changes. Customer supply does not eliminate assembly and calibration fees.
Quote for industrial control PCBA assembly: describe the application, existing configuration, and expected quantity so we can discuss assembly inclusions and selection requirements.