Engineering Reference Configuration
LED strip SMT assembly: assembly configuration and test deliverables
The following adjustable engineering configurations support material, functional, and process review; they are not stocked models or commitments to current production-line capabilities. Approved fabrication documentation and order acceptance requirements govern.
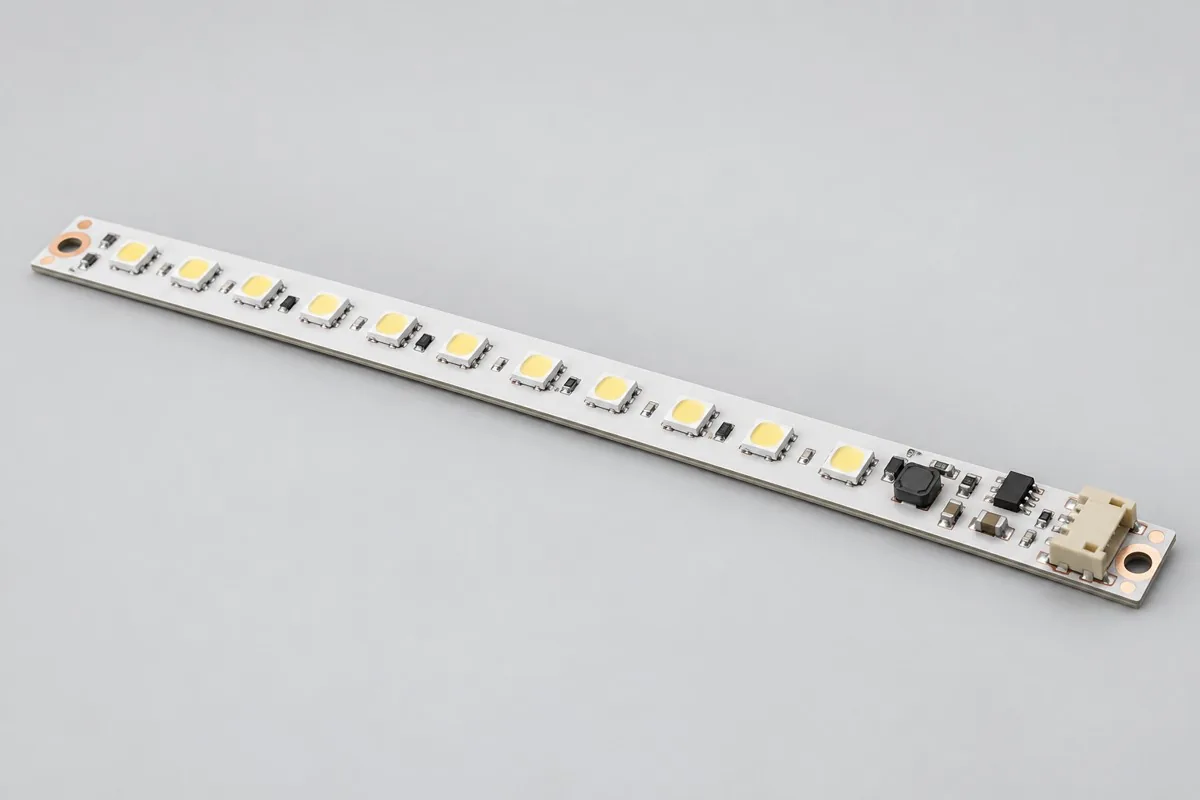
LED strip SMT assembly supports contract manufacturing and procurement review for linear lighting, segmented series connections, and color-temperature options. First confirm LED series/parallel networks, optional segment interfaces, soldered-wire/board-to-board connections, external constant-current driver options, and aluminum-core or FR-4 boards selected by thermal paths and installation. Then compare single-sided SMT → optical-bin verification → wire soldering → illumination testing scope and acceptance costs for polarity, per-segment current/illumination, color differences, and thermal measurement points. This page separates LED board + LED lots/bins + optical/electrical test records from T5/T8/linear-light layout options with drawing-defined lengths, helping determine whether quotations cover the actual application. Quotation documentation reference:BOM · bare board · material supply
Reference specification and configuration options
| Options | Reference Configuration |
|---|---|
| Power and Logic Domains | Low-voltage constant-current driver input; current determined by LED combinations |
| Functional Module | Linear lighting, segmented series connections, and color-temperature options |
| Core Components/Architecture | LED series/parallel networks; optional segment interfaces |
| Interface and Channels | Soldered-wire/board-to-board connections; external constant-current driver options |
| Board Layers and Material Options | Aluminum-core or FR-4 boards; selected by thermal paths and installation |
| Component types | 2835/other specified LEDs; connectors or soldered wires |
| Assembly Route | Single-sided SMT → optical-bin verification → wire soldering → illumination testing |
| Material Supply Scope | LED brand/part number/color temperature/brightness bin locked; other components sourced with authorization |
| Firmware and Parameters | LED strips without firmware; separately list revisions for included dimming modules |
| Test Focus | Polarity, current/illumination of each segment, color variation, and thermal test points |
| Deliverables | LED board + LED lots/bins + optical/electrical test records |
| Configuration Limits/Options | T5/T8/linear-light layout options; lengths per drawings |
How much does LED strip SMT assembly cost, and what is included?
LED brands, part numbers, color-temperature/brightness bins, LED counts, and aluminum-core or FR-4 bare boards affect strip pricing. Itemize single-sided placement, bin verification, wire soldering, segment illumination, and optical/electrical tests. Constant-current drivers, power supplies, and housings absent from BOMs should not be included in LED-board unit prices.
Quotation terms depend on the approved files, quantity, material supply, tests and delivery requirements.
Prepare a structured RFQ or use the short inquiry form.
| Cost Item | Scope for This Configuration | Billing frequency and work scope | Procurement Verification |
|---|---|---|---|
| Bare PCB and core components | LED series/parallel networks; optional segment interfaces; aluminum-core or FR-4 boards selected by thermal paths and installation | Price according to actual bare-board/component purchase quantities; authorize critical components and substitutions individually | LED brand/part number/color temperature/brightness bin locked; other components sourced with authorization |
| Placement and Post-Assembly | Single-sided SMT → optical-bin verification → wire soldering → illumination testing | Feeder/program setup per lot; assembly priced per board, joint, or process as agreed, with counting rules specified | 2835/other specified LEDs; connectors or soldered wires |
| Manufacturing Preparation | Review stencils, first articles, and support tooling against the actual assembly route | New stencils/carriers may be separate one-time charges; verify panelization, revision, and condition before reuse | Reduced quantities do not automatically eliminate first-article or feeder setup |
| Functional Support | Polarity, current/illumination of each segment, color variation, and thermal test points | Itemize test-method/fixture/script setup; agree execution charges per board, channel, or test duration | Separate supporting development from execution records for each board |
| Software and Parameters | LED strips without firmware; separately list revisions for included dimming modules | When firmware exists, distinguish file programming/verification from software development; omit programming without a firmware revision | Customer-approved files, parameters, and readback rules determine scope |
| Delivery and Change | LED board + LED lots/bins + optical/electrical test records; T5/T8/linear-light layout options; lengths per drawings | Price accessories, retesting, and revision changes by approved work items; do not prefill fixed rates | Check BOM, tooling, programs, and acceptance revisions before reorders |
Should LED strips use aluminum-core or FR-4 boards?
Select by thermal density, mounting interfaces, and cost. Aluminum-core boards provide thermal-conduction structures but still require housings and thermal interfaces. FR-4 suits configurations with acceptable thermal conditions. Compare complete thermal paths and connections, beyond board-material prices.
| Comparison Metric | Current Conditions | Factors Influencing Procurement Decision |
|---|---|---|
| Manufacturing Delivery | Single-sided SMT → optical-bin verification → wire soldering → illumination testing | Produce boards/assemblies per BOM and assembly drawings; this does not establish that every system function passes |
| Functional Acceptance | Polarity, current/illumination of each segment, color variation, and thermal test points | Compare unit prices after defining test stimuli, limits, accessories, and records; review missing test inputs first |
| Configuration Options | Soldered-wire/board-to-board connections; external constant-current driver options; aluminum-core or FR-4 boards selected by thermal paths and installation | Confirm circuit/program compatibility before reviewing assembly and test costs for interface, stackup, or component changes |
| Delivery Scope | T5/T8/linear-light layout options; lengths per drawings | Complete-system accessories, application development, and project verification are not automatically included in board assembly |
How should LED strip length, LED count, and color temperature be selected?
Determine series/parallel connections from mounting dimensions, constant-current drivers, and lighting targets; lengths follow drawings. Manage color temperature, brightness bins, and lots together. More LEDs also change power and heat requirements; package names such as 2835 do not establish identical efficacy.
- First list required linear lighting, segmented series connections, and color-temperature options, distinguishing build-to-print manufacturing, configuration adjustments, and new-function development.
- Then freeze complete part numbers for LED series/parallel networks and optional segment interfaces, soldered-wire/board-to-board connections, external constant-current driver options, and aluminum-core or FR-4 boards selected by thermal paths and installation. Separate customer-supplied and sourced materials: LED brand/part number/color temperature/brightness bin locked; other components sourced with authorization.
- Use first articles to check single-sided SMT → optical-bin verification → wire soldering → illumination testing and firmware-free LED strips; list included dimming-module revisions separately. If only program files are supplied, agree programming verification first; development requires separate review.
- Convert polarity, per-segment current/illumination, color differences, and thermal measurement points into acceptance items with stimuli, limits, and records; specify fixture ownership, per-board execution, and post-repair retesting.
- Finally confirm LED board + LED lots/bins + optical/electrical test records and T5/T8/linear-light layout options with drawing-defined lengths. Compare totals using identical quantities, accessories, and test scope, then freeze the order revision.
Applicable uses and situations requiring separate review
Linear light strips, device internal lighting.
Small high-power point sources, regulated automotive lamps, and direct-mains drivers require different designs. Without defined constant-current drivers, currents, and thermal interfaces, do not quote complete-lamp performance from nominal LED power.
Assembly Challenges for This Product
Control long-panel support, LED polarity, and depaneling stress together. Do not mix unapproved brightness/color-temperature bins. Stencils and reflow must prevent lens/package damage. After wire soldering, perform pull/visual checks before illuminating each segment.
Structural, thermal, and configuration trade-offs
Aluminum-core boards simplify thermal-path design but still require thermal interfaces and housings. FR-4 suits low-thermal-density, cost-sensitive configurations. Plug-connected segments simplify repairs; soldered wires save height, but their contact voltage drops and fastening differ.
Product-specific test matrix
| Test stage | Inspection/Functional Methods | Acceptance Record |
|---|---|---|
| Electrical Segmentation | Check polarity, current, and voltage drop per segment under approved drivers | Segment number, power condition, and result |
| Optical Consistency | Compare brightness and color differences using specified geometry/equipment | LED level, measurement conditions and data |
| Thermal installation | Observe hot spots using specified thermal bases and drive conditions | Interface/base version and temperature logs |
Defect Handling and Acceptance
Check reversed LEDs, mixed bins, cracked joints, and detached wires separately. Acceptance defines dim-LED, color-difference, and current conditions. Agree the optical measurement method, equipment, geometry and records for each project before quoting or accepting test coverage.
LED strip PCB assembly: material supply and revision management
Retain complete LED ordering numbers and bin labels with lots. Count customer-supplied LEDs by bin; sourcing must not ignore color tolerance and brightness bins simply because color temperatures match. If drivers and wires do not ship with boards, state test configurations.
Prototyping vs. Production Differences
Samples verify LED spacing and thermal contact. Production assembles separate bins in separate lots, uses fixtures to control constant current and optical positioning, and reinspects end LEDs and connection joints after depaneling.
Delivery Configuration
LED board + LED lots/bins + optical/electrical test records. T5/T8/linear-light layout options; lengths per drawings.
Convert this configuration into a reviewable order
For linear LED strip orders, check complete LED part numbers/bins, BOM, pick-and-place files, DNP lists, quantity, material supply, series/parallel and driver arrangements, and thermal drawings. This page's firmware-free strips need no programming files; supply programs only for revisions adding dimming modules with commissioned programming. Separate costs for LED supply, single-sided placement/stencils, wire soldering/depaneling, and optical/electrical/thermal test resources under approved drivers and measurement geometry. Reapprove bin or structural changes; list delivery milestones after material readiness and scheduling.
| Required project inputs | Engineering Decisions Affected | Records/delivery as agreed in the order |
|---|---|---|
| LED part numbers, bins and color temperature | List complete LED part numbers, bins, and series/parallel connections to determine mixing restrictions and optical-verification resources. | Deliver LED lots/bins, illumination, and current records; measure color temperature under agreed instrument conditions. |
| LED Strip Heat Dissipation Assembly | Provide constant-current drivers and actual heat sinks/thermal-interface materials. | Link thermal records to assembly conditions; tests without heat sinks cannot predict complete-lamp lifetime. |
LED strip assembly processing common issues
How much does LED strip SMT assembly cost, and what is included?
For standard placement, first calculate board quantity × billable points per board × price per point + setup fee. A project-specific quotation requires review of the available files, quantity, materials, requested tests, delivery destination, taxes, shipping, and trade terms. This is a placement-only reference; bare PCBs, materials, and testing are charged separately. Any formula on this page organizes cost inputs; it is not a quoted rate.View cost items, calculation conditions, and sources.
Should LED strips use aluminum-core or FR-4 boards?
Select by thermal density, mounting interfaces, and cost. Aluminum-core boards provide thermal-conduction structures but still require housings and thermal interfaces. FR-4 suits configurations with acceptable thermal conditions. Compare complete thermal paths and connections, beyond board-material prices.
How should LED strip length, LED count, and color temperature be selected?
Determine series/parallel connections from mounting dimensions, constant-current drivers, and lighting targets; lengths follow drawings. Manage color temperature, brightness bins, and lots together. More LEDs also change power and heat requirements; package names such as 2835 do not establish identical efficacy.
Why do LED SMT prices differ with identical LED counts?
Brands/bins, board materials, segment connections, and test scope differ. Align complete LED part numbers, color-temperature bins, drive conditions, and delivered lengths before comparing placement and optical/electrical inspection costs.
Can LED strip lighting guarantee no color difference?
Illumination checks primarily identify polarity and opens; color differences also require LED-bin and agreed optical-condition checks. Link segment-current and thermal-point results to lots; visible illumination alone is insufficient for release.
Can T5 and T8 strips be converted by changing board length alone?
Recheck housings, power supplies, LED series/parallel arrangements, and installation. Form-factor names do not determine all electrical parameters. Revision quotations distinguish changes to bare boards, LED counts, connections, and verification.
What lot documentation should be retained for sourced LED strips?
Retain brands, part numbers, color-temperature/brightness bins, and lots, linked to segment-current and optical/electrical records. Mixed bins affect visual consistency; equal LED packages cannot replace bin management.
How should electrical-segment testing be included in LED strip procurement acceptance?
The reference method checks polarity, current, and voltage drop per segment under approved drivers. Records include segment identifiers, supply conditions, and results. Supply test inputs, applicable configurations, and acceptance limits with the inquiry, then agree first-article verification and per-board execution scope. Price test-resource setup separately from each execution. Methods can be reviewed before limits are available, but completing an operation does not establish specification compliance.
How should optical-consistency testing be included in LED strip procurement acceptance?
The reference method compares brightness and color differences using specified geometry/equipment. Records include LED bins, measurement conditions, and data. Supply test inputs, applicable configurations, and acceptance limits with the inquiry, then agree first-article verification and per-board execution scope. Price test-resource setup separately from each execution. Methods can be reviewed before limits are available, but completing an operation does not establish specification compliance.
How should thermal-installation testing be included in LED strip procurement acceptance?
The reference method observes hot spots using specified thermal bases and drive conditions. Records include interface/base revisions and temperatures. Supply test inputs, applicable configurations, and acceptance limits with the inquiry, then agree first-article verification and per-board execution scope. Price test-resource setup separately from each execution. Methods can be reviewed before limits are available, but completing an operation does not establish specification compliance.
Do firmware-free LED strip assembly quotations still require programming charges?
This page covers firmware-free strips; list revisions separately if dimming modules are included. When the actual BOM has no programmable components, programming should not be a default charge. Added control or dimming functions require separate circuit, program, and test revisions before comparing additional work.
What costs require reconfirmation when LED strip assembly changes LED bins or panelization?
Components are 2835/other specified LEDs with connectors or soldered wires. Supply requirements lock LED brand/part number/color temperature/brightness bin; other parts may be sourced with authorization. Bin changes first require review of original color-difference/current test conditions; panel changes require stencil, alignment, and depaneling review. Existing stencils and lot bins cannot be carried over automatically. Quote new resources separately from per-board optical/electrical tests; accept LED boards separately from assemblies with optical structures.
How should total LED strip assembly costs be compared when critical components are customer-supplied and others sourced?
Create a procurement-responsibility table with LED brand/part number/color temperature/brightness bin locked and other components sourced with authorization. Confirm complete part numbers, quantities, packaging, and remaining-material rules with deliveries. Customer supply changes only procurement boundaries; single-sided SMT → optical-bin verification → wire soldering → illumination testing and polarity, per-segment current/illumination, color differences, and thermal measurement points remain actual work. Approve shortage, substitution, or lot-change impacts first; do not directly compare consigned assembly unit prices with material-inclusive assembly totals.
What requires retesting after LED strip repairs or repeat orders?
Select retests by change impact. Original acceptance covers polarity, per-segment current/illumination, color differences, and thermal measurement points; shipping records include LED board + LED lots/bins + optical/electrical test records. Repairs affecting power, interfaces, critical analog circuits, or software revisions require related tests, beyond repaired joints. Repeat orders must align with original BOMs, parameters, and test resources. Agree retest charges by approved items and actual quantities; do not assume free service or fixed turnaround.
Are panelized LED strip SMT quotations calculated per panel or per strip?
Confirm delivered strip lengths, panel layouts, LED counts, connection methods, and post-depaneling illumination records. Prepare stencils and feeders for approved panels. Placement may be priced per placement/panel/strip, but conversions must state strips per panel. Define optical-bin and segment-current checks by actual delivery units so low panel prices do not conceal omitted depaneling, wire soldering, or testing.
Compare Other Products in This Category
- Automotive Low-Voltage LED Lighting Board: Drivers, thermal interfaces, and optical/mechanical relationships.
When initial design files must be created
RGBW four-channel constant-current color-mixing control board design: Provides access to corresponding circuits/layouts and verification plans. Channels, interfaces, or mechanics may differ from this page's engineering reference and require independent design revisions. Design-stage deliverables include source files, BOMs, layout constraints, and verification records. Assembly procurement on this page delivers actual PCB assemblies/components, programmed revisions, and product-test records against approved files.
Return to LED PCB assembly configuration comparison · Component Supply and Procurement · Testing and Delivery Scope
Material and Process Reference
- Engineering reference | SMT packages and assembly methods: pads, stencils, and thermal processes: a package/assembly method index only; not evidence that the product configurations on this page are models produced by KFPCBA
- Engineering reference | Soldering processes and defect isolation: wetting, residues, and solder oxidation: a reference entry for soldering, residues, and defect isolation methods only. Verify this page's soldering routes against specific materials/components